Carburising behaviour, core hardness, hardenability and cost — a practical comparison for gear procurement engineers.
2026-08-26 · Dişli Bilgisi
Most gear steel arguments end the same way: 20CrMnTi for carburised gears, 42CrMo for larger sections or induction-hardened parts. The reasoning behind that rule is worth understanding, because it decides cost, distortion and lead time long before the first chip is cut.
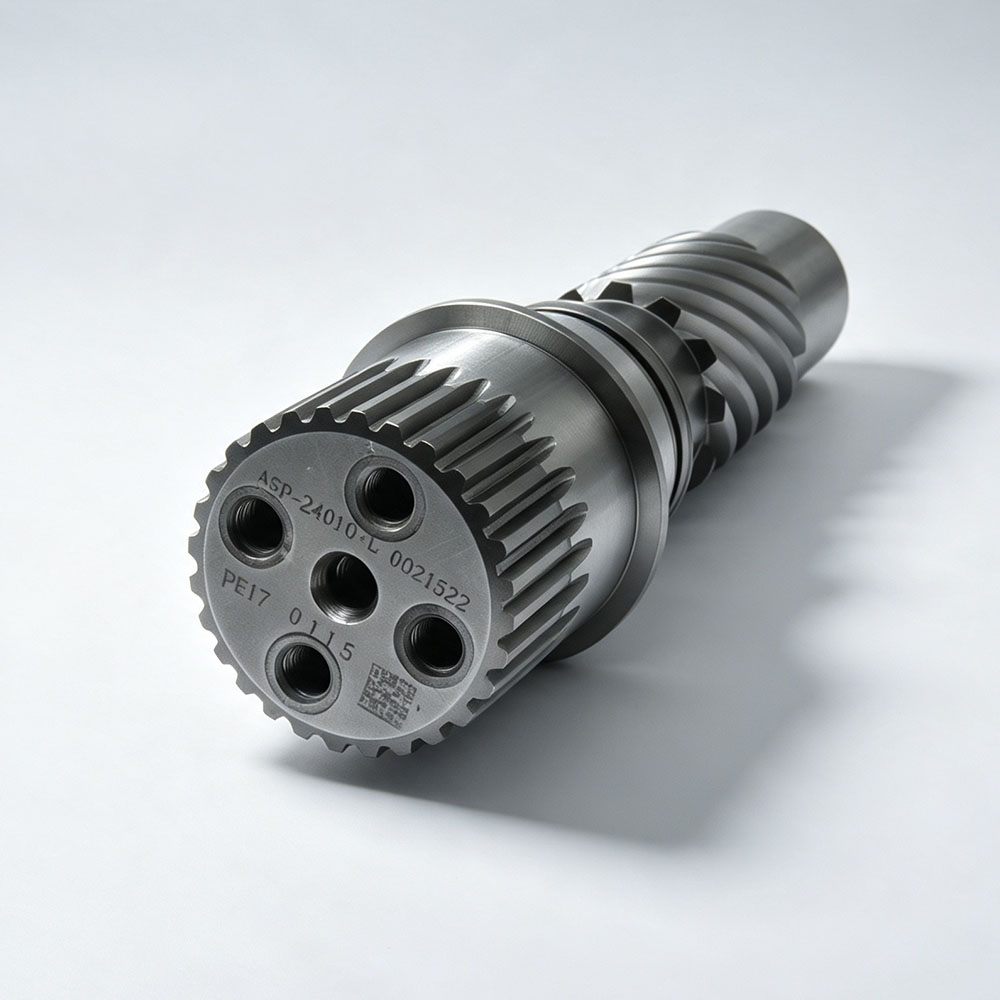
20CrMnTi is a low-carbon carburising steel. After carburising and quenching it gives a hard case (typically 58–62 HRC) over a tough core of roughly 30–40 HRC — exactly the combination a gear tooth wants: wear resistance on the flank, ductility at the root. It forges well, machines predictably, and is widely available in China at low cost, which is why planetary gears and shaft gears are almost always made from it.
42CrMo is a medium-carbon, higher-hardenability steel. It does not need carburising: quench and temper gives a through-hardened part with strength that holds up in thick sections where 20CrMnTi would not harden fully. Cross shafts, large flanges and heavily loaded shafts are typical applications. It machines harder and distorts more during heat treatment, so grinding allowance has to be planned properly.
A practical rule: if the tooth surface needs a hard case with a soft core, choose 20CrMnTi-type steel; if the whole section must carry strength and the part is thick, choose 42CrMo-type. For export programs, confirm that the specified grade is accepted by the end customer's material standard before tooling — substituting steel after PPAP approval is expensive for everyone.